Tag: Material Selection

  • The Best Material Is Not Always the Most Expensive: A Product Development Lesson in Low-Cost Engineering

    The Best Material Is Not Always the Most Expensive: A Product Development Lesson in Low-Cost Engineering

    When developing a product, it is easy to fall into a familiar assumption:

    If we want a better result, we should use a better material.

    If we want a stronger structure, we upgrade the material.

    If we want the electronics to be thinner, we choose a more advanced circuit solution.

    If we want the product to feel more premium, we add more parts, more processes, and more cost.

    But after working on enough real-world products, I have become increasingly convinced that this is not always the right way to think.

    Sometimes, a very ordinary — even seemingly “low-end” — material can create an unexpectedly refined result when it is used in exactly the right place.

    The important question is not how sophisticated the material is.

    The important question is:

    What problem do you actually need it to solve?

    A Lighting Problem Inside a Flexible Structure
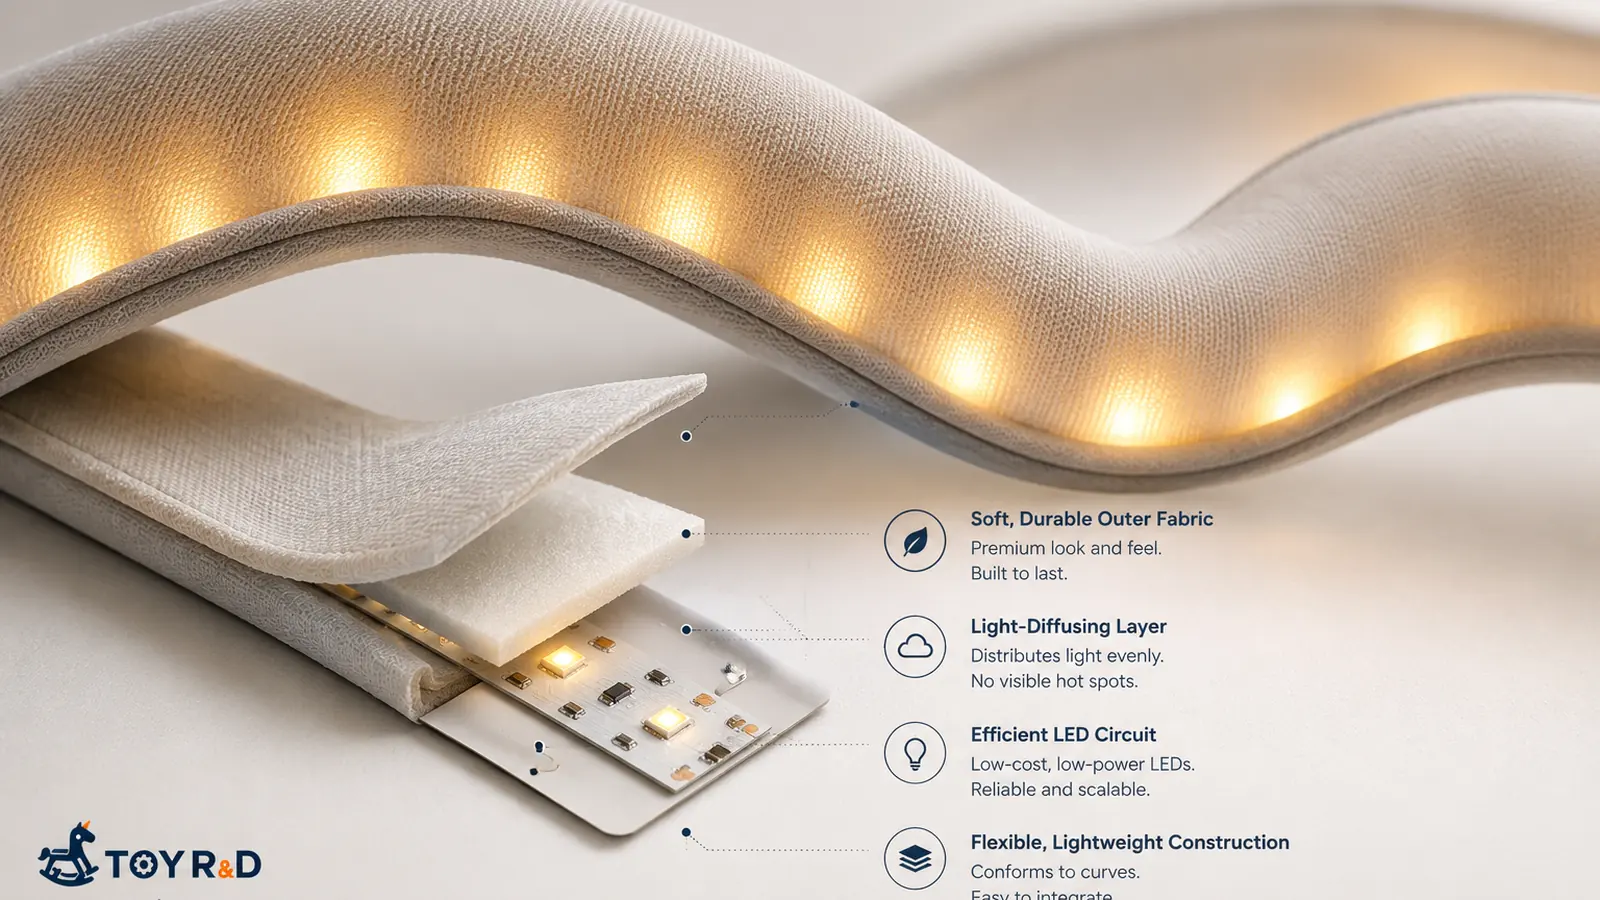
    Soft textile structure opened to show a light-diffusing layer and low-cost LED circuit that create a flexible lighting effect.
    The solution should meet the real bending, lighting, weight, and cost requirements—nothing more.

    In one project, we needed to add a lighting effect inside a soft, flexible textile structure.

    From an electronics perspective, this did not seem particularly complicated.

    If a structure needs to bend while carrying multiple LEDs, one of the most obvious solutions is:

    Use a flexible printed circuit, or FPC.

    That is exactly what FPC is designed for.

    It is thin, flexible, suitable for mounting LEDs, and technically easy for an electronics engineer to justify.

    On paper, it looks like the standard answer.

    But product development is different from pure electronics engineering.

    A technically correct solution is not always the best product solution.

    So we went back and looked at the actual requirements again.

    Did the structure really need a full flexible circuit?

    Did it need to survive repeated, extreme folding?

    Did it require high-density routing?

    High-speed signals?

    Very tight dimensional tolerances?

    Not really.

    The real requirements were much simpler:

    • It needed to carry LEDs.
    • It needed to conduct electricity.
    • It needed to tolerate a certain degree of bending with the textile structure.
    • It needed to stay lightweight.
    • It had to remain hidden inside the product.
    • And it had to be inexpensive.

    Once the requirements were broken down this way, the problem changed.

    We were no longer asking:

    “What is the best flexible circuit solution?”

    We were asking:

    “What is the lowest-cost structure that can reliably meet these actual requirements?”

    Those two questions sound similar.

    But they can lead to very different answers.

    A Solution That Did Not Look “Premium”

    The final solution was not a conventional high-spec flexible circuit.

    Instead, we used a very low-cost circuit structure built on a substrate that naturally offered a useful degree of flexibility.

    By itself, the material was not impressive.

    It was not something a marketing team would put on the front of the package.

    The end user would probably never know it existed.

    But inside the right product structure, it did exactly what we needed.

    The LEDs could be distributed along the flexible section.

    The overall assembly could still bend sufficiently.

    The electronics could remain hidden inside the textile construction.

    And the user could still clearly perceive the intended lighting effect.

    What the customer experienced looked more sophisticated than what the internal cost structure might suggest.

    That is one of the most interesting things about product development.

    The user experiences the result, not the BOM.

    “Cheap” Does Not Mean “Bad”
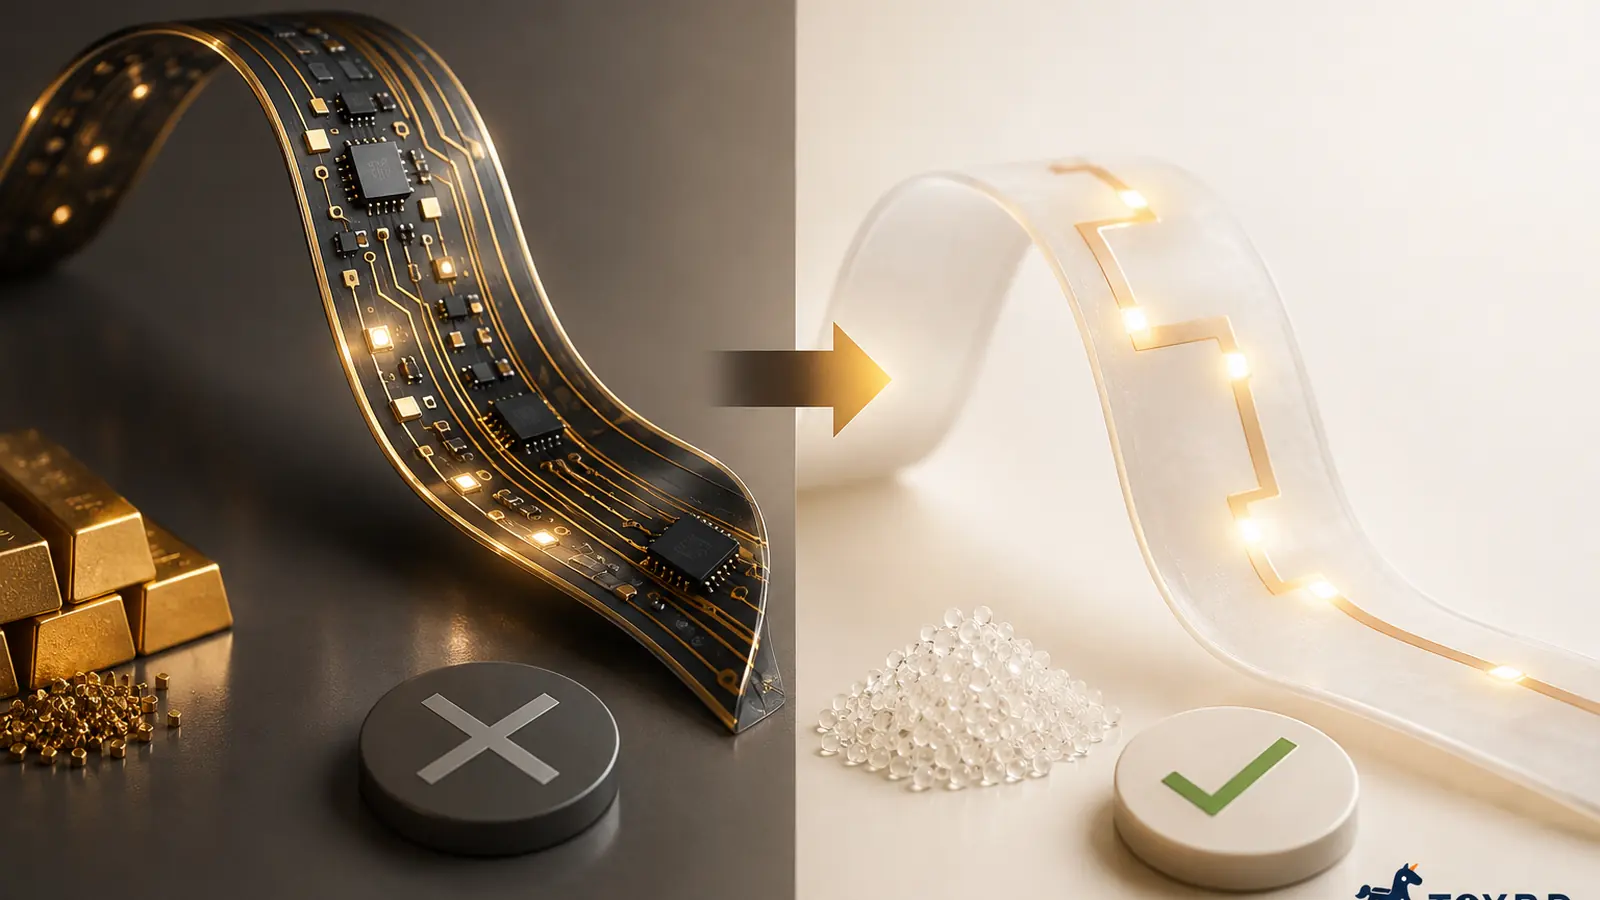
    Comparison of a high-spec flexible circuit with a simpler low-cost circuit structure that still delivers the required lighting effect.
    A lower-cost structure is valuable when it reliably delivers the performance the product genuinely needs.

    There is an important distinction here.

    Cost optimization is not simply about finding a cheaper component.

    If you replace a two-dollar part with a one-dollar part but create more failures, more assembly difficulty, more rework, more compliance risk, or more after-sales problems, that is not real cost optimization.

    Good cost engineering means:

    Finding a lower-cost solution that still satisfies the performance the product genuinely requires.

    In some cases, a simpler and cheaper structure may even be more suitable for mass production than a supposedly “better” solution.

    That is why I do not find it particularly useful to divide materials into:

    premium materials and low-end materials.

    A better distinction is:

    the right material and the wrong material.

    Do Not Choose the Material First and Justify It Later

    Engineers naturally tend to begin with the technologies they already know.

    An electronics engineer sees a flexible structure and thinks of FPC.

    A mechanical engineer sees a connection problem and thinks of screws, snap-fits, or reinforcement ribs.

    A supplier sees an appearance issue and may immediately suggest painting, UV printing, IMD, or another added component.

    None of these solutions are necessarily wrong.

    The problem is that we sometimes move too quickly into how to build something before clearly defining what the product actually needs.

    A useful habit in product development is to ask, before choosing the solution:

    What conditions does this feature truly need to satisfy?

    Then break those conditions down.

    For example:

    How much does it actually need to bend?

    How many bending cycles does it need to survive?

    Can the user touch this component?

    What is the realistic product life requirement?

    Is the feature carrying a functional load, or is it mainly creating a visual effect?

    Is this level of performance genuinely required by the product, or was it added by the engineering team simply because it was possible?

    A surprising amount of unnecessary cost enters a product before these questions have been properly answered.

    Premium Products Do Not Always Come From Expensive Parts
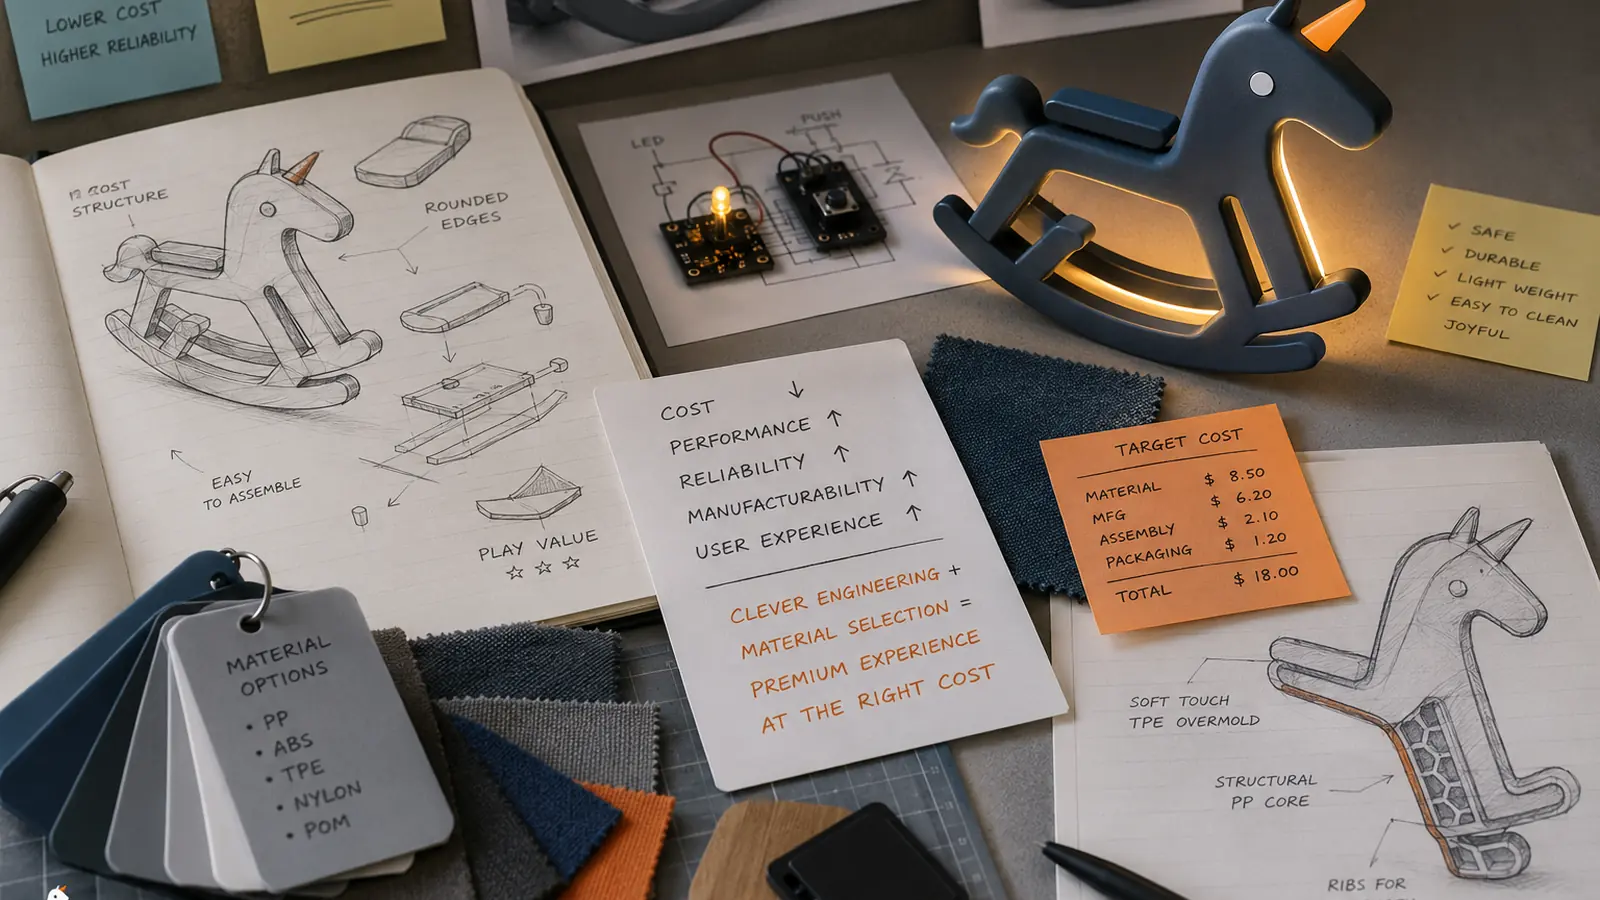
    Toy design sketches, material samples, a lighting prototype, and cost notes showing how thoughtful engineering creates value at the right cost.
    The best material decision is the one that creates the intended experience without spending where the customer gains no value.

    I increasingly enjoy studying products that are clever on the outside and surprisingly simple on the inside.

    They create strong perceived value without relying on excessive material cost.

    In many ways, that is harder than simply using expensive components.

    Because good product engineering is not:

    “I know an advanced technology, so I should put it into the product.”

    It is:

    “I know many possible technologies, but I will only use the one this product actually needs.”

    That is why opening a well-designed mass-produced product can sometimes create a strange reaction:

    “That is all there is to it?”

    But this kind of simplicity is rarely accidental.

    It is often what remains after many rounds of trade-offs, simplification, testing, and decision-making.

    A ToyRD Product Development Principle

    At ToyRD, these are exactly the kinds of engineering decisions I want to keep documenting.

    Not simply:

    Which material is the best?

    Which chip is the most advanced?

    Which manufacturing process is the most sophisticated?

    But rather:

    What is the most reasonable choice when cost, performance, reliability, manufacturability, and user experience all have to be balanced at the same time?

    Great products are not always great because they use expensive things.

    Often, they are great because someone understood precisely:

    where the money should be spent — and where it should not.

    Sometimes, a very ordinary material, used in exactly the right place, can create a surprisingly extraordinary result.

    That may be one of the most interesting parts of product development.
  • When Cheap Plastic Becomes Expensive: A PP vs. ABS Lesson from a Moving Toy Mechanism

    When Cheap Plastic Becomes Expensive: A PP vs. ABS Lesson from a Moving Toy Mechanism

    *Some product details in this case have been generalized to protect project confidentiality.*

    In toy development, material cost is easy to see.

    Engineering cost is not.

    A resin that saves a few cents per part can look like a good decision in a BOM review. But when that material is used inside a mechanism with gears, sliding parts, repeated movement, and tight dimensional relationships, the real cost may appear later—in noise, friction, inconsistent assembly, rework, tooling changes, and delayed production.

    Recently, I ran into exactly this kind of problem on a toy project involving a small motorized mechanism.

    The mechanism itself was not complicated. A motor drove a gear train, and the gear train moved a plastic component back and forth repeatedly. But the motion depended on several molded parts staying within the right dimensional range.

    At an early stage, PP was selected for part of the mechanism as a cost-saving option.

    On paper, that choice looked reasonable.

    In practice, it became much more complicated.

    PP Is Not a Bad Material

    PP, or polypropylene, is one of the most widely used plastics in toys and consumer products.

    It is lightweight, cost-effective, chemically resistant, and tough. It works very well in many applications such as housings, living hinges, containers, clips, and flexible parts.

    The problem is not that PP is "cheap" or "low quality."

    The problem is that material selection has to match the job the part is doing.

    For a decorative cover, a small dimensional change may not matter much.

    For a moving mechanism, it can matter a lot.

    The Real Problem Was Dimensional Stability

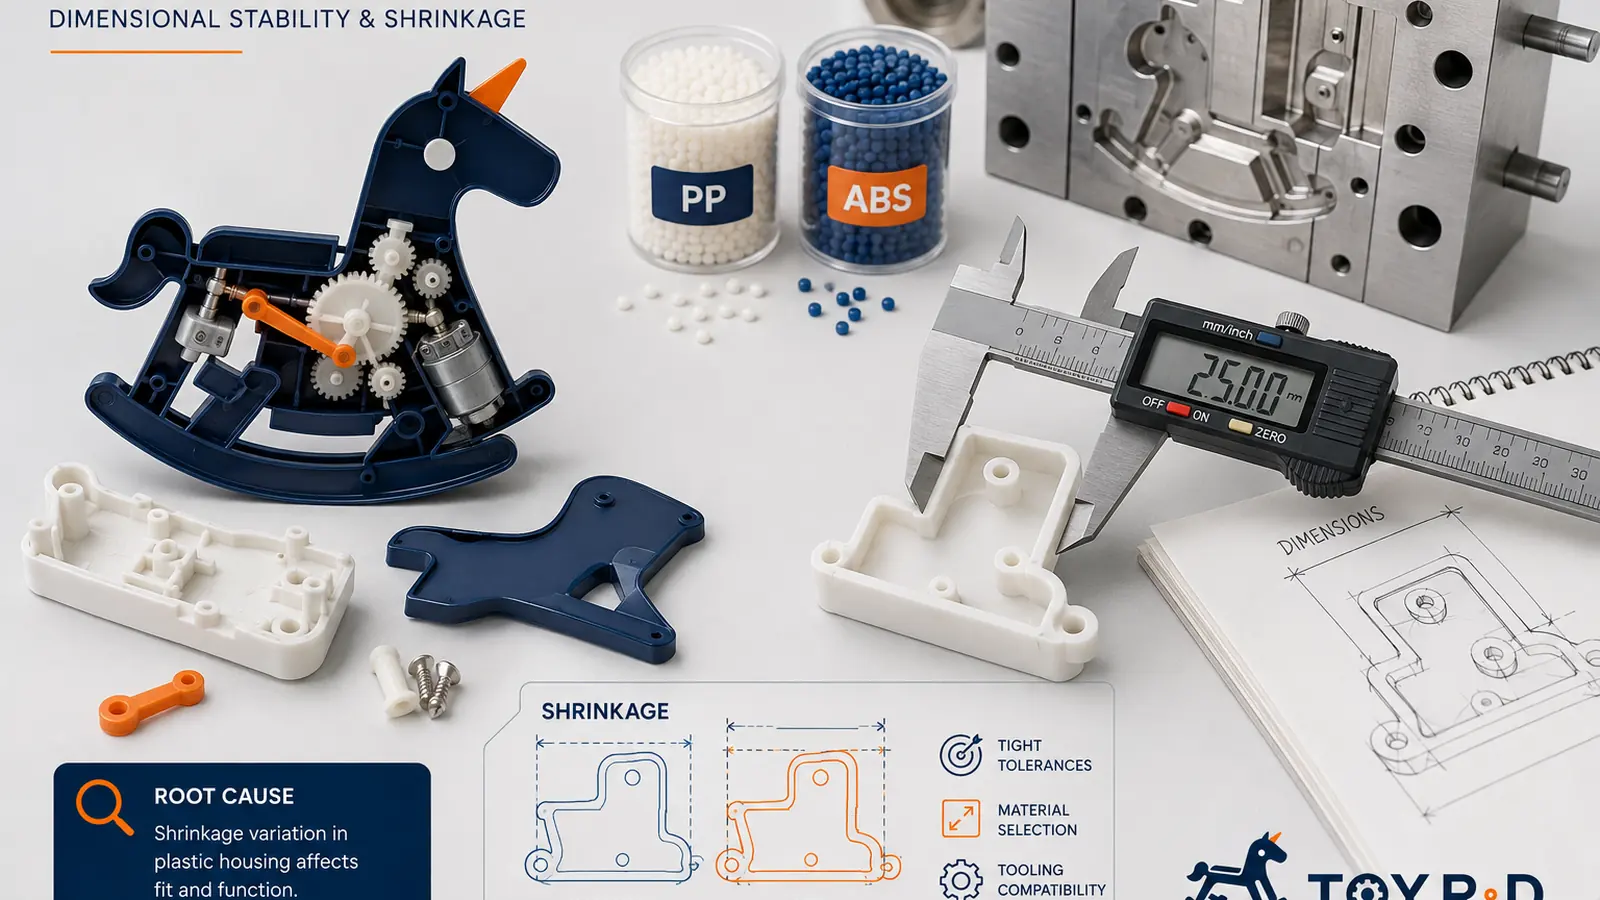
    Moving toy mechanism components, ABS and PP materials, a mold, and measuring tools used to investigate shrinkage and dimensional stability.
    Material shrinkage and dimensional stability must be evaluated as a mechanism-level issue.

    One of the most important differences between PP and ABS is molding shrinkage.

    The exact value depends on the resin grade, filler content, wall thickness, mold temperature, packing pressure, gate design, and many other processing conditions. So it is never correct to treat shrinkage as one universal number.

    But the general engineering trend is clear:

    PP typically has significantly higher molding shrinkage than ABS.

    That becomes important when molded parts are part of a mechanical system.

    A mechanism may rely on:

    • gear center distances,
    • shaft positions,
    • sliding clearances,
    • guide surfaces,
    • wall straightness,
    • bearing locations,
    • part-to-part gaps,
    • and cumulative tolerance across several components.

    A small deviation in one part may be harmless.

    Small deviations across several parts can become a system-level problem.

    That is where symptoms such as these begin to appear:

    • intermittent friction,
    • unstable movement,
    • increased mechanical noise,
    • inconsistent assembly,
    • higher motor load,
    • parts rubbing where they should not,
    • and units that behave differently even though they use the same design.

    This is a good reminder that a plastic part does not exist independently.

    Inside a mechanism, every dimension interacts with another dimension.

    A Cheaper Resin Can Create More Expensive Problems

    When engineers or sourcing teams review a BOM, the conversation often focuses on the material price itself.

    For example:

    Can we save a little by changing this part from ABS to PP?

    That is a valid question.

    But it is incomplete.

    The better question is:

    What happens to the total engineering cost if this material changes?

    That total can include:

    • tooling adjustment,
    • additional sampling,
    • longer debugging cycles,
    • extra assembly labor,
    • sorting and rework,
    • higher QC burden,
    • reduced yield,
    • mechanical noise complaints,
    • inconsistent function,
    • and production delays.

    If a material saves $0.03 per unit but causes $0.08 per unit in additional manufacturing or quality cost, that is not cost reduction.

    It is cost transfer.

    And cost transfer is often harder to see because it appears across different departments.

    "Why Not Just Switch the Existing Mold to ABS?"

    Once a PP part starts creating dimensional problems, the obvious reaction is often:

    Then let's just mold the same tool in ABS.

    Sometimes that can work.

    But it should not be treated as a drop-in material substitution.

    Injection molds are designed around the expected behavior of the material, including shrinkage.

    The tool cavity dimensions, part dimensions, clearances, draft, ejection strategy, and processing window were all developed under certain assumptions.

    If a mold was designed around a higher-shrinkage PP grade and the material is suddenly changed to a lower-shrinkage ABS grade, the final dimensions can shift.

    That may affect:

    • overall part size,
    • fit with mating parts,
    • gear alignment,
    • snap engagement,
    • interference,
    • sliding gaps,
    • and ejection behavior.

    The correct conclusion is not:

    "A PP mold can never run ABS."

    That would be too absolute.

    The correct conclusion is:

    A material change after tooling must be treated as an engineering change, not a purchasing change.

    The mold, part dimensions, tolerances, processing conditions, and mechanical performance all need to be re-evaluated.

    Then Another Idea Came Up: Filled PP

    During the discussion, another possibility came up:

    Could we keep PP, but use a modified grade with talc, mineral filler, or glass fiber to improve stiffness and reduce shrinkage?

    From a material-science perspective, this is a perfectly reasonable direction to investigate.

    Filled PP compounds are widely used in industry precisely because fillers can improve properties such as:

    • stiffness,
    • dimensional stability,
    • heat resistance,
    • creep performance,
    • and molding shrinkage.

    So the proposal is technically plausible.

    But technically plausible is not the same as production-ready.

    The existing mold was not originally developed around an arbitrary filled PP grade.

    Changing filler type and percentage can also change:

    • melt flow,
    • viscosity,
    • warpage behavior,
    • surface appearance,
    • abrasion on tooling,
    • ejection behavior,
    • weld-line behavior,
    • and actual molded dimensions.

    At the same time, the molding team raised practical concerns about whether a different compound could create new molding or release problems in the existing tool.

    At that point, the most useful response was not to argue from theory.

    It was to test.

    This Is Where AI and Factory Experience Should Meet

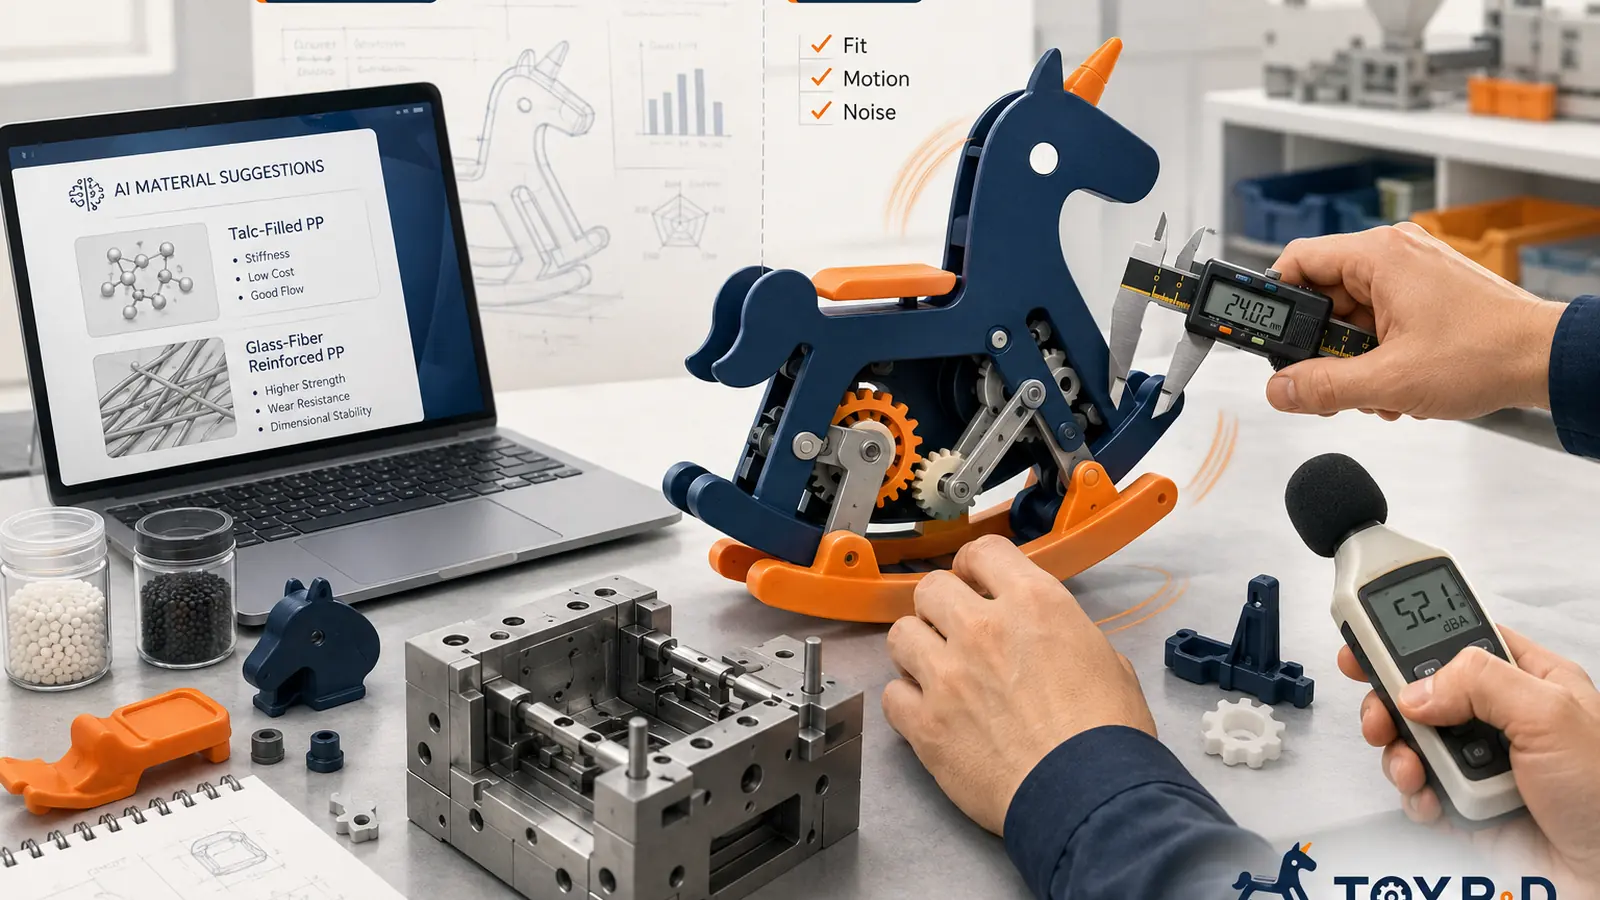
    Moving toy mechanism being checked for fit, motion, and noise beside material suggestions, a mold, and measurement tools.
    Use trials and measurements to test material hypotheses against the real tool and mechanism.

    This case also illustrates something increasingly common in product development.

    AI can very quickly suggest technically reasonable directions:

    • use a filled PP grade,
    • reduce shrinkage,
    • increase stiffness,
    • change a material system,
    • adjust clearances,
    • review processing parameters.

    That is useful.

    But AI does not physically see the mold.

    It does not automatically know:

    • the actual draft angle,
    • the tool surface condition,
    • the gate location,
    • the wall-thickness transitions,
    • the ejector layout,
    • the existing dimensional deviation,
    • the real machine settings,
    • or what happened during the previous molding trials.

    Factory technicians and tooling engineers, on the other hand, often carry years of experience that is difficult to express in a datasheet.

    They may look at a tool and say:

    "I don't like this material change on this mold."

    That statement may not come with a full polymer-science explanation, but it may still be based on many past failures.

    So who should you trust?

    The better answer is:

    Do not turn it into a competition.

    A stronger development process looks like this:

    1. AI or engineering analysis expands the possible solution space. 2. Tooling and molding teams identify practical risks. 3. Controlled material trials are run. 4. Critical dimensions are measured. 5. Parts are assembled into the real mechanism. 6. Noise, load, movement, temperature, and durability are evaluated. 7. The decision is made using production evidence.

    AI is useful for generating hypotheses.

    Factory experience is useful for identifying hidden risks.

    Testing decides whether either one is right for the actual product.

    PP Can Also Create Surface-Treatment Challenges

    There is another PP-related issue that is easy to underestimate: surface treatment.

    PP is a low-surface-energy plastic.

    That means printing, painting, labeling, and adhesive bonding can be more difficult than on materials such as ABS unless the material, ink, adhesive, or surface preparation is designed for it.

    Depending on the product, manufacturers may use:

    • flame treatment,
    • corona treatment,
    • plasma treatment,
    • primer,
    • special inks,
    • special adhesives,
    • or modified resin grades.

    On a previous project, we also explored laser marking on PP.

    For that specific application, the result was quite acceptable.

    That does not mean every PP grade can be laser-marked well. Laser performance depends heavily on resin formulation, color, additives, wavelength, and process settings.

    But it reinforces the same lesson:

    A simple material change can affect much more than the injection molding step.

    It may also affect decoration, marking, adhesion, assembly, appearance, and long-term production consistency.

    So Should Moving Toy Mechanisms Avoid PP?

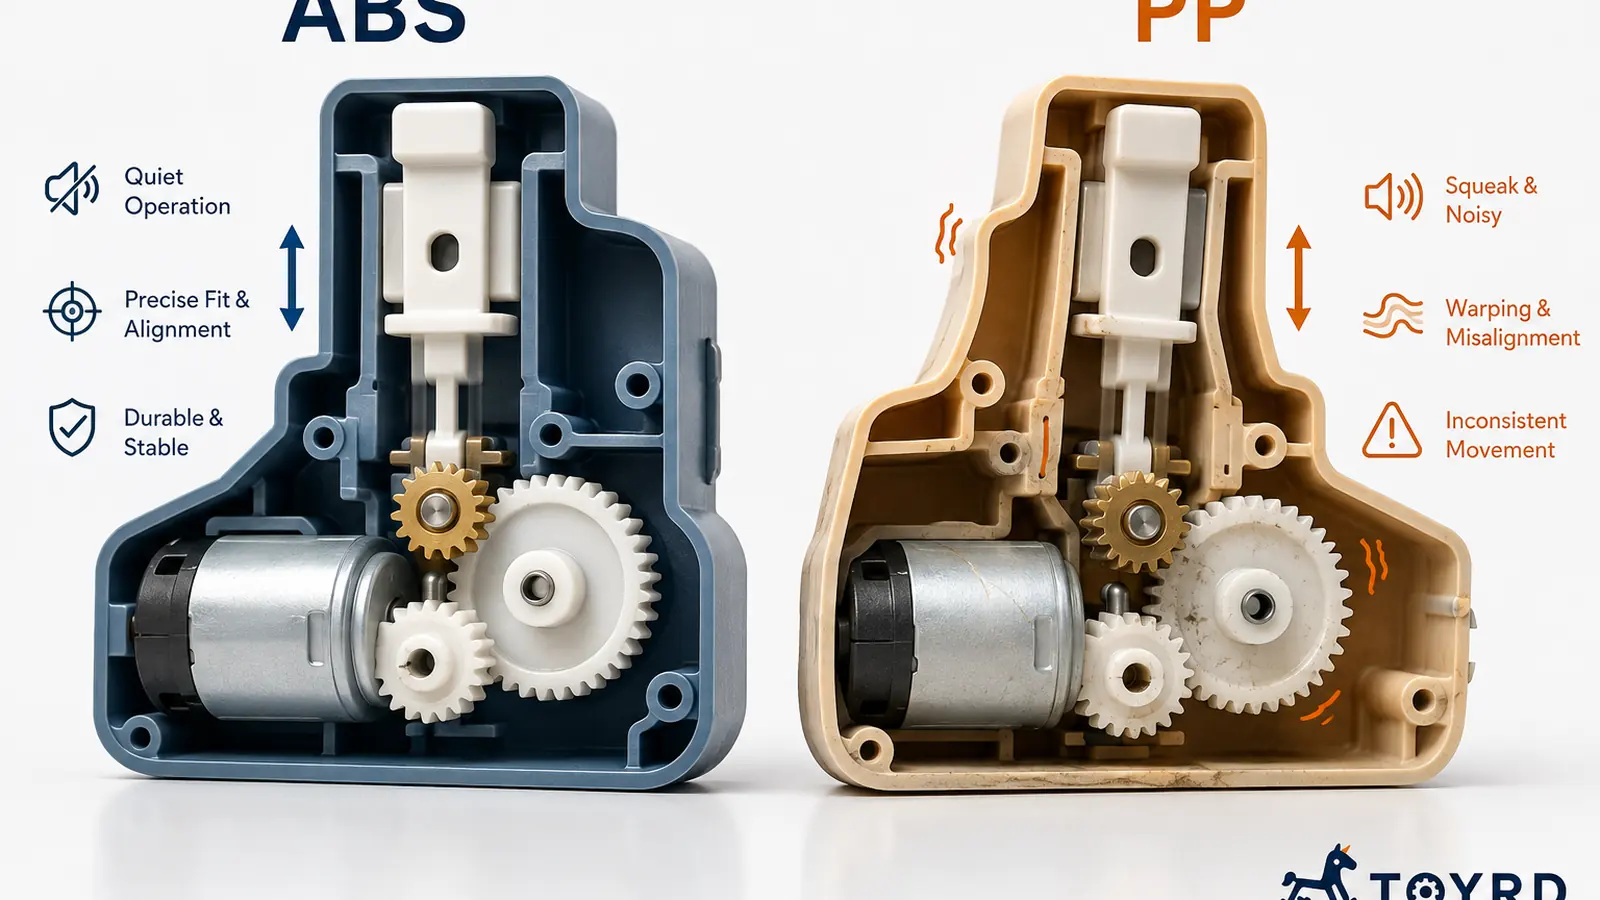
    Comparison of ABS and PP housings for the same moving toy mechanism, showing the effects on noise, fit, alignment, and stability.
    A lower resin price does not help if movement, fit, and production consistency become harder to control.

    No.

    That would be too simplistic.

    PP is successfully used in many moving products, automotive systems, home appliances, hinges, gears, guides, and mechanical components.

    The important lesson is different:

    Do not choose PP for a precision-sensitive moving mechanism only because it is cheaper.

    If the component has any of the following characteristics, material selection deserves more attention:

    • gear positioning,
    • sliding movement,
    • reciprocating motion,
    • tight dimensional chains,
    • noise sensitivity,
    • alignment-critical features,
    • multi-part assemblies,
    • or narrow functional clearances.

    In those cases, ABS can often be a more conservative starting point when dimensional stability and predictable molding behavior matter more than squeezing out the lowest possible resin cost.

    And if PP is still the preferred material, it is better to decide that at the beginning of the project.

    Then you can define:

    • the exact PP grade,
    • whether it is filled or unfilled,
    • expected shrinkage,
    • tool compensation,
    • critical tolerances,
    • sliding clearances,
    • warpage limits,
    • and worst-case tolerance stack.

    That is material engineering.

    Changing resin after tooling and hoping everything else remains the same is not.

    One of the Most Expensive Questions in Toy Development

    A question I hear often in product development is:

    Can we make this part a little cheaper?

    Sometimes the answer is absolutely yes.

    But for moving structures, I increasingly prefer a different question:

    If we save money here, where might we pay for it later?

    That small change in mindset can prevent a surprising amount of trouble.

    Material cost is visible.

    Debugging cost is not.

    A BOM may show that PP is cheaper than ABS.

    It does not show the extra two weeks spent chasing noise, movement inconsistency, dimensional drift, or molding problems.

    That is why I increasingly think about Total Engineering Cost, not just part cost.

    ToyRD Note

    This is exactly the kind of development lesson I want to document on ToyRD.com.

    A material datasheet can tell you the shrinkage range of PP.

    An AI system can suggest talc-filled or glass-fiber-reinforced PP.

    A tooling engineer may tell you the existing mold is unlikely to like the change.

    All three inputs can be useful.

    But real product development happens where materials, tooling, mechanism design, supplier experience, and physical testing meet.

    The most useful question is often not:

    "What is the shrinkage rate of PP?"

    It is:

    "I already have a molded PP mechanism that is noisy and dimensionally unstable. What is the lowest-risk way to recover the project?"

    That is a much harder question.

    And that is the kind of question ToyRD is built around.

    ToyRD.com — Practical toy development notes from real engineering problems.